
Description
What Is DBB Valve?
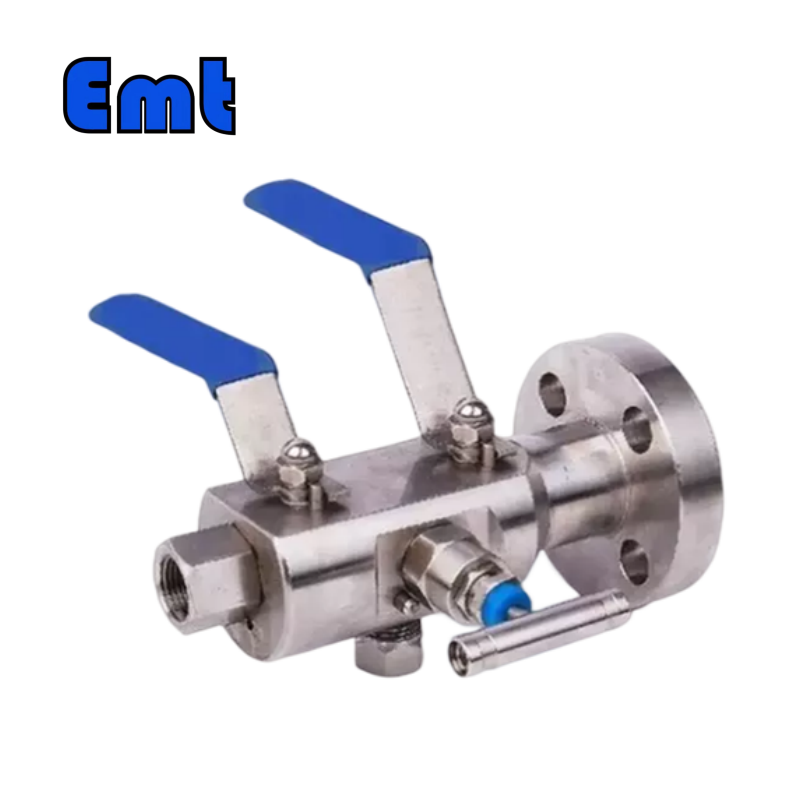
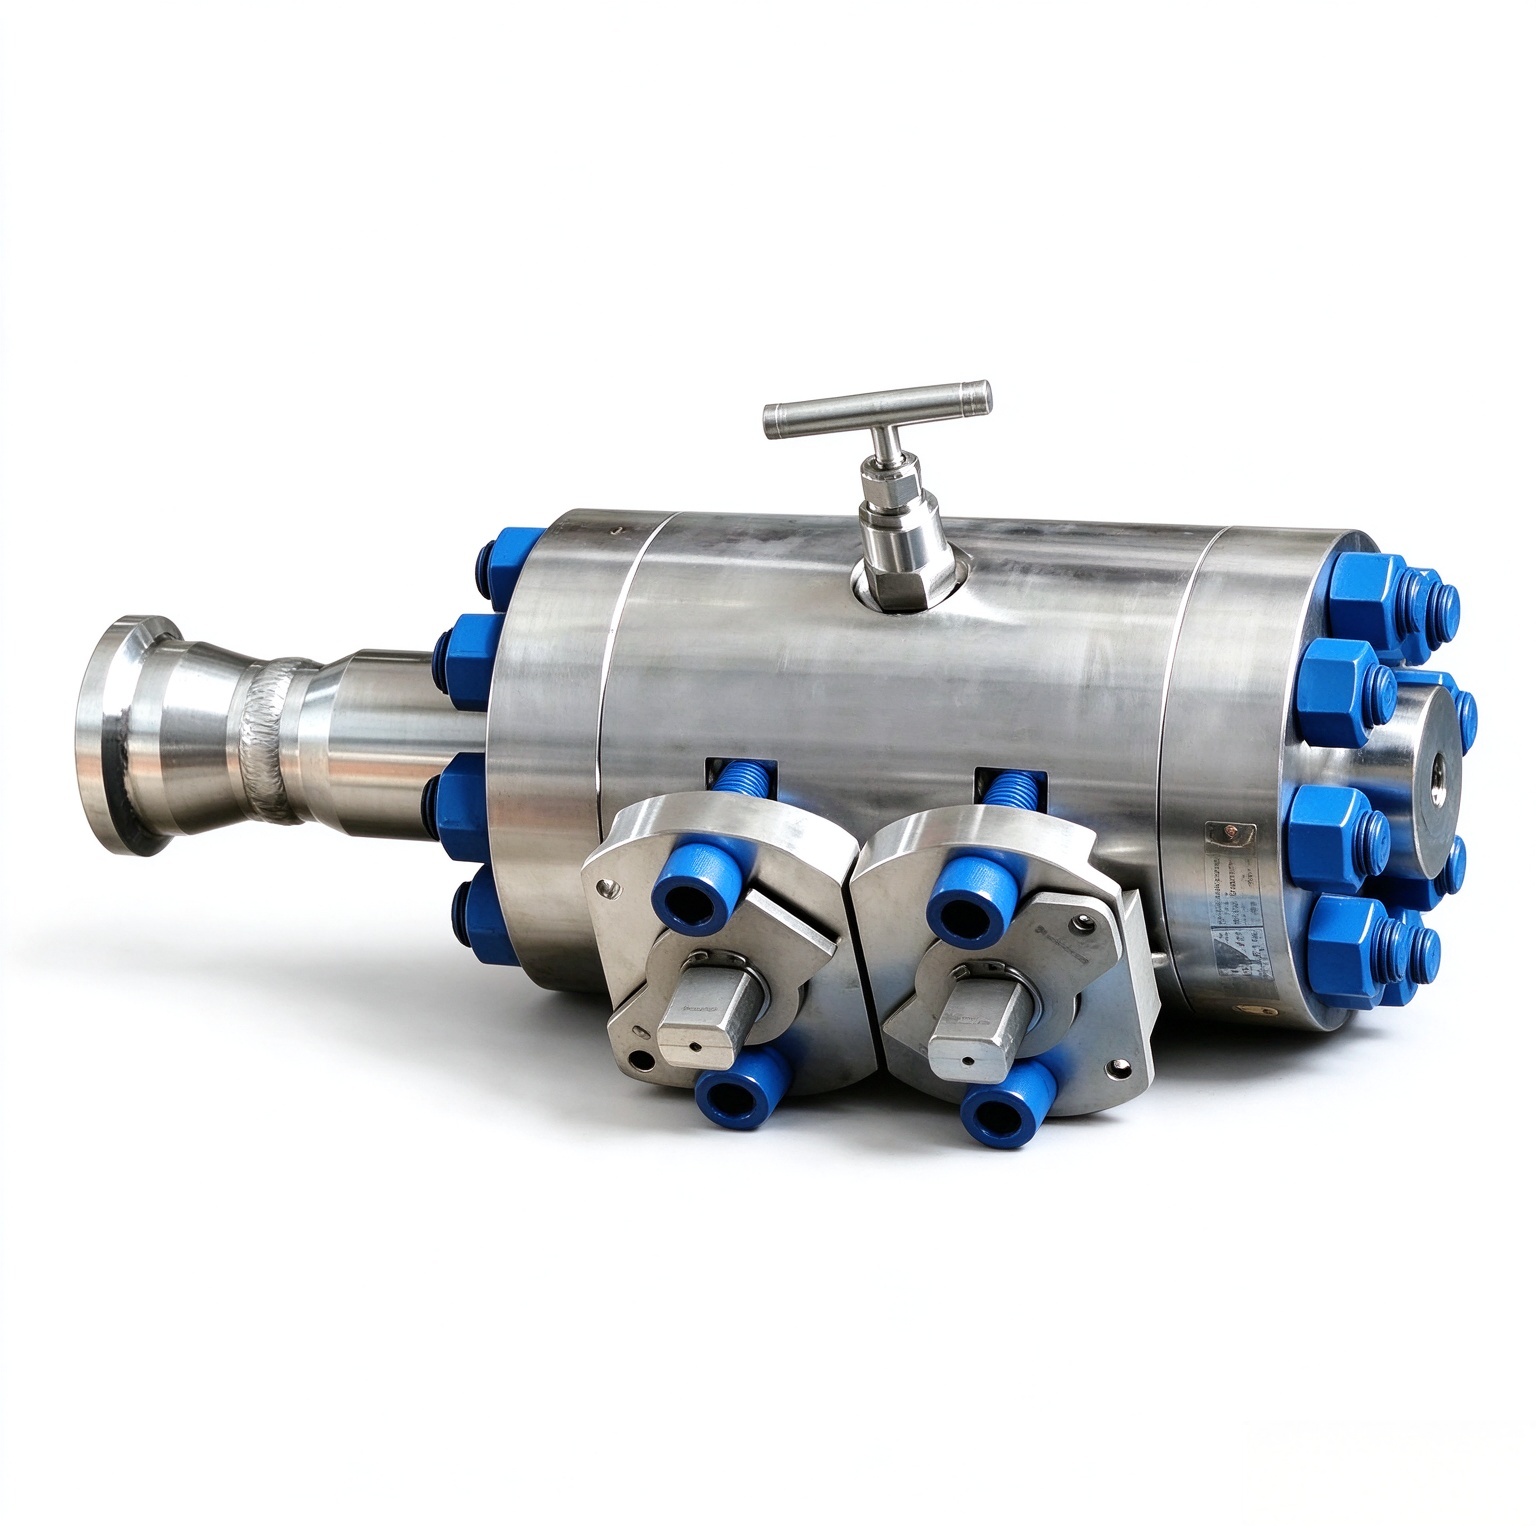
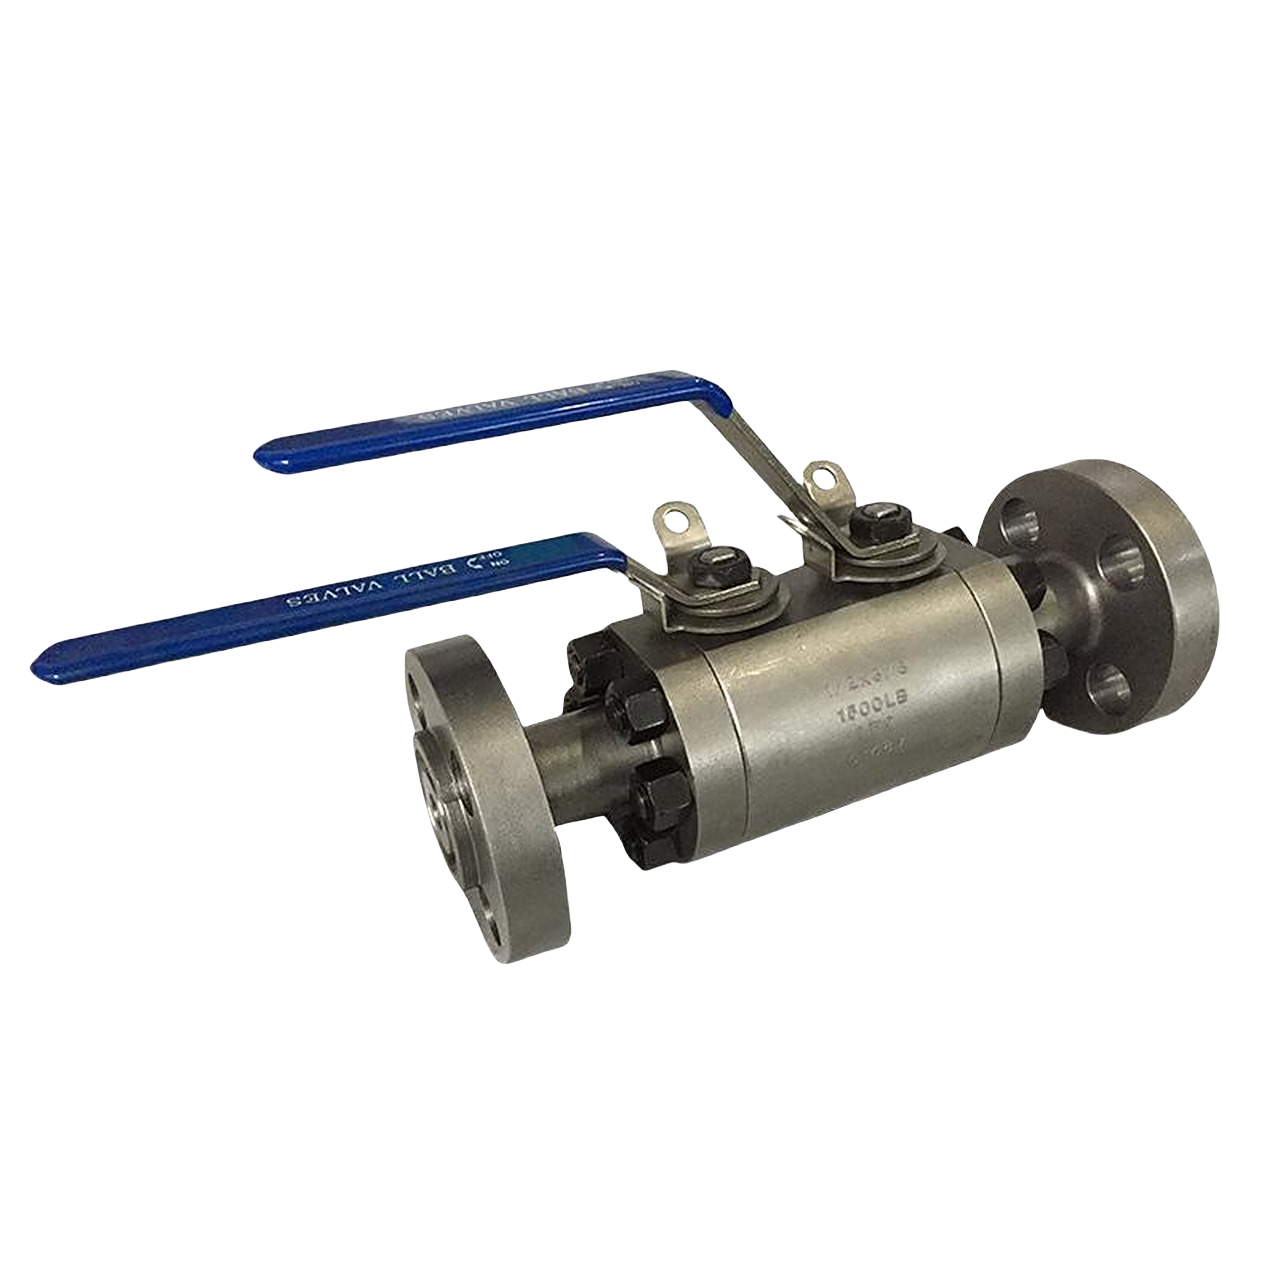
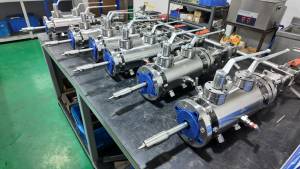
As a DBB valve manufacturer, EMT produces the double block and bleed valve (DBB valve) used to control fluid flow in pipeline equipment. A DBB valve combines two blocking elements with a bleed path in one body. This design isolates a section of the line and vents trapped pressure between the seals. In our equipment, the DBB valve is fitted to pig signallers. It allows operators to remove or replace a signaller while the pipeline stays under pressure. This removes the need to drain line media before maintenance, which raises both safety and efficiency.
What Are the Key Parameters?
The DBB valve is defined by its isolation layout, its bleed function, and the way it connects to the pig signaller assembly. The double block arrangement gives two independent barriers against line pressure, while the bleed port lets trapped fluid or gas escape before work starts. Because the valve serves a removable pig signaller, it must hold pressure reliably and release cleanly. EMT supplies the valve as part of the equipment assembly, together with a simple retriever and two fully threaded studs. Exact dimensions, pressure ratings, and materials are set per project and per pipeline service. We confirm these against the application during engineering review rather than assuming them.
| Parameter | Value | Note |
|---|---|---|
| Valve type | Double block and bleed (DBB) | Two blocking elements plus a bleed path |
| Function | Isolate and vent under pressure | Supports online signaller maintenance |
| Application | Pig signaller isolation | Pairs with removable pig signaller |
| Bleed path | Integrated vent | Drains trapped pressure between seals |
| Supplied with | Simple retriever and two fully threaded studs | Part of the equipment assembly |
| Materials | Forged steel, ASME-rated | Confirmed per project service |
| Quality program | ASME U Stamp | Manufactured under certified control |
How Does It Work?
The DBB valve forms two series seals and opens an intermediate bleed path. Once both blocking elements shut, they retain upstream line pressure. The bleed port discharges all fluid and gas trapped within the cavity between the two seals.Once that cavity reads zero, the pig signaller can be removed without exposing the operator to live line pressure. This is why the valve is central to safe, in-service maintenance.
Where Should You Use It?
Use the DBB valve wherever a pig signaller must be serviced while the pipeline keeps running. Typical scenarios include high-pressure pipelines and lines carrying hazardous media, where draining down is slow, costly, or unsafe. It also suits routine signaller replacement, inspection, and troubleshooting, because the line stays online and production is not interrupted. The valve integrates into the wider pigging system, working alongside the launcher, receiver, and main line valve. Operators gain a controlled isolation point that simplifies maintenance and supports safe work permits. For any pipeline where uptime and operator safety both matter, the DBB valve is the practical choice.
Why Choose This Design?
- Two barriers plus a bleed deliver safer isolation than a single block valve.
- Operators service pig signallers under pressure, so the line stays online.
- Online maintenance cuts downtime and avoids draining costly line media.
- Integrated bleed removes trapped pressure before any work begins.
- Supplied with a simple retriever and two fully threaded studs.
- Built under ASME U Stamp quality control for dependable pressure service.
Who Is EMT and Why Trust Us?
EMT is an oil and gas pipeline equipment manufacturer serving pipeline operators and EPC contractors. We design and build pigging equipment, signallers, and valve assemblies for demanding field conditions.We as a DBB valve manufacturer produced under an ASME U Stamp quality program, so fabrication and pressure integrity are controlled to recognized code requirements. We follow ASME, NACE, and API conventions in design, material selection, and testing.
Our team supports projects from specification through delivery. We review each application, confirm the valve configuration against the pipeline service, and supply the assembly with the retriever and threaded studs needed for installation. We also attend industry exhibitions, where we meet operators and contractors face to face and share our latest pipeline equipment. That direct contact keeps our designs aligned with real field needs.
If you are sourcing a dependable DBB valve, send us your line conditions and signaller details. Our engineers will recommend the right configuration and provide a quotation. Visit emt-pipe.com or contact EMT to discuss your project.
FAQ
What is a DBB valve used for?
A DBB valve isolates a section of pipeline and bleeds trapped pressure between two seals. On our equipment, it lets operators remove or replace a pig signaller while the line stays under pressure.
Can a pig signaller be removed under pressure with a DBB valve?
Yes. The double block and bleed design isolates the signaller and vents trapped pressure first. This allows safe removal and replacement without draining line media.
Is EMT a certified DBB valve manufacturer?
EMT manufactures DBB valves under an ASME U Stamp quality program. We follow ASME, NACE, and API conventions for pipeline equipment.
Related Products
- Removable Pig Signaller — pairs with the DBB valve for under-pressure signaller removal.
- Pig Signaller — intrusive indicator that shows pig position in the line.
- Pig Launcher and Receiver — barrel systems for launching and receiving pipeline pigs.
Reviews
There are no reviews yet.